

Flexible circuits offer advantages that rigid PCBs cannot, including improved reliability, reduced weight, and the ability to fit into compact or dynamic applications. However, these benefits often come with manufacturing considerations that can influence the overall cost of the finished circuit.
Everything from material selection and layer count to stiffeners, coverlay construction, and design complexity plays a role in determining price. By understanding how these design choices affect manufacturing, engineers can optimize both performance and cost before production begins.
From a product manager and engineering perspective, the most effective way to control cost is during the design phase. Once a design is finalized and released, options become limited, and changes become expensive. By evaluating key design choices early, engineers can make informed decisions that balance performance requirements with practical manufacturing constraints.
Material Choices and Their Impact on Cost
Material selection is one of the biggest drivers of price in flex PCB manufacturing. Even small changes in material type, thickness, or specification can have a measurable impact on both cost and lead time.
Thicker flex materials, for example, are inherently more expensive. As material thickness increases, so does the complexity of processing. Materials at or above 100 microns often require additional handling considerations and may extend lead times. In many cases, thinner constructions can meet the same functional requirements at a lower cost.
Another common cost driver is the use of name-brand materials. Well-known suppliers such as DuPont or Panasonic offer proven performance, but specifying these materials explicitly can limit sourcing flexibility, especially for offshore manufacturing. Allowing equivalent materials where appropriate can open up more options and reduce both cost and lead time without sacrificing quality.
Cosmetic choices can also quietly add cost. Non-standard colors for soldermask, coverlay, or silkscreen often require special processing or materials. Unless there is a clear functional or branding requirement, sticking with standard colors is the most cost-effective approach.
Copper weight is another key factor. Heavier copper, especially beyond 2 ounces, increases plating requirements and processing time. This not only raises cost but can also affect yield and lead time. For many designs, standard copper weights are sufficient and provide a better balance between performance and manufacturability.
Stiffener selection also plays a role. FR4 and polyimide stiffeners are widely used and readily available, making them cost-effective options. Alternatives such as stainless steel or aluminum may offer specific mechanical or thermal benefits, but they introduce additional cost and complexity. Even within FR4, non-standard thicknesses or materials can lead to higher pricing.
For rigid-flex designs, the impact of material selection becomes even more pronounced. Non-standard thicknesses, specialty laminates, or exotic materials can quickly increase both cost and lead time. Whenever possible, aligning with standard material sets used by the manufacturer helps keep pricing under control.
Design Decisions That Influence Pricing
Beyond materials, the physical design of the flexible circuit board has a direct impact on cost. One of the most straightforward factors is size. Larger designs require more material and reduce the number of parts that can fit on a production panel. Smaller designs, when practical, allow for better panel utilization and lower cost per unit.
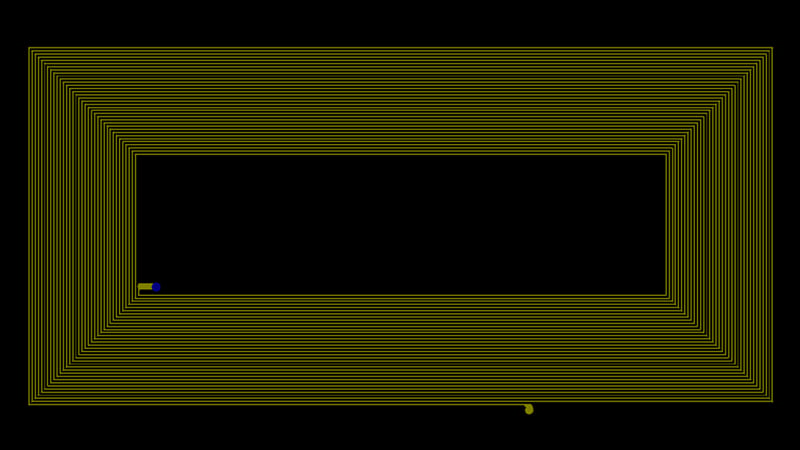
An example of a flexible circuit board designed to be a coil and lay flat.
Panelization strategy is closely tied to this. If an array is required, maximizing the number of circuit boards per panel is critical. Efficient panel layouts reduce material waste and improve throughput. However, this must be balanced with manufacturability. Overly dense arrays or poorly designed breakaway features can create handling issues and reduce yield.
Technology requirements are another major cost driver. Pushing the limits of fabrication capabilities often leads to higher pricing. For example, extremely fine trace widths in the range of 0.002 to 0.003 inches may be achievable, but they require tighter process control and can increase scrap rates. Similarly, very small vias, such as 0.004 inches, typically require laser drilling, which adds both time and cost.
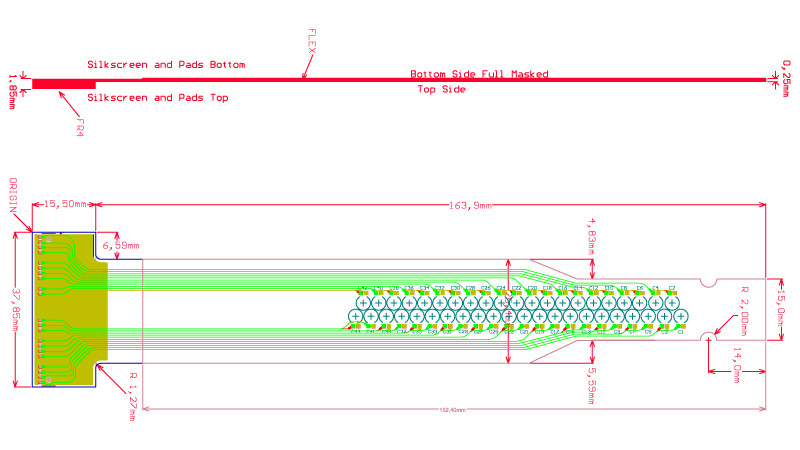
A flexible PCB design that relays signals from the pads to various pads where capacitors will be attached.
Layer count and construction also play a role. While adding layers can solve routing challenges, it increases complexity and material usage. In flex designs, additional layers can also reduce flexibility, which may not align with the original design intent.
The required build class is another consideration. Class 2 is the most common and is suitable for a wide range of applications. Moving to Class 3 introduces stricter inspection criteria and tighter tolerances, which naturally increases cost. While Class 3 is necessary for high-reliability applications, it should only be specified when required.
Surface finish selection can also influence pricing. Standard finishes such as ENIG are widely available and cost-effective. More specialized finishes, including ENEPIG or hard nickel-gold, provide additional performance benefits but come at a higher cost. These should be used only when the application demands them.
Balancing Cost and Performance
It is important to recognize that not all cost drivers can or should be eliminated. Some design requirements are dictated by the application and cannot be compromised. The goal is not to remove costs entirely, but to understand where flexibility exists.
In many cases, small adjustments can lead to meaningful savings. Reducing copper weight, selecting standard materials, or slightly modifying board size can have a cumulative effect on overall cost. These changes often do not impact performance but can improve manufacturability and yield.
The most effective approach is collaboration. Working with your PCB manufacturer early in the design process allows you to identify cost drivers before they become fixed. Manufacturers can provide insight into standard material sets, preferred panel sizes, and process limitations that may not be obvious during design.
Summary
While some flex PCB design changes are unavoidable, it is always best to watch for any chances to reduce costs. The items in this blog post are not all-encompassing, so it can be important to work with your manufacturer from the beginning to keep costs down and find other ways to reduce costs whenever possible. Even if something seems expensive, consulting your manufacturer can sometimes reveal possibilities you may not have considered.
By making informed choices early and aligning designs with standard manufacturing practices, engineers can significantly reduce cost without compromising performance. The key is to approach design with both functionality and manufacturability in mind, and to engage with manufacturing partners throughout the process to identify opportunities for optimization.
Key Takeaways
- Material selection has a major impact on cost, with thicker materials, heavy copper, and non-standard options increasing both price and lead time.
- Allowing material equivalents and using standard colors and finishes can help reduce costs without affecting performance.
- Board size and panelization efficiency directly influence cost, with smaller and well-optimized designs offering better value.
- Advanced fabrication requirements such as fine traces, small vias, and higher build classes increase complexity and pricing.
- Early collaboration with your PCB manufacturer is the most effective way to identify cost-saving opportunities and ensure a balanced, manufacturable design.